Low Exotherm Epoxy Potting Compound Selection Guide
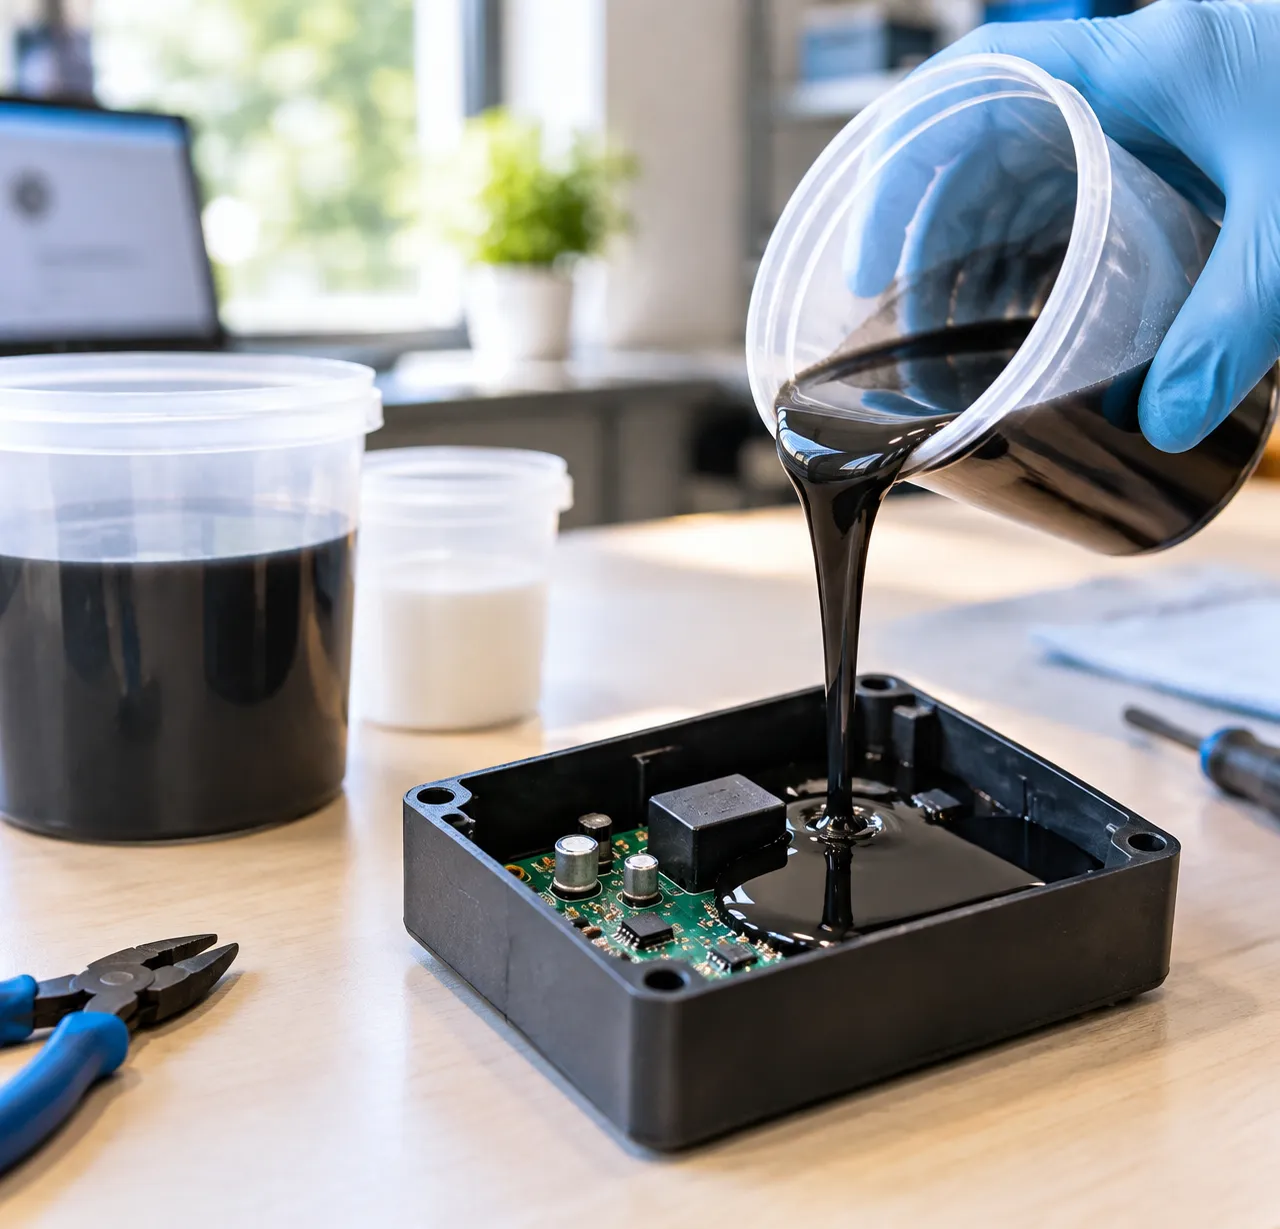
Potting thick electronic assemblies without frying sensitive components is a major challenge.
When high-volume pours cure too quickly, the resulting heat spike can easily crack housings, damage delicate circuitry, and ruin your yields.
The fix? Choosing the right low exotherm epoxy potting compound.
In this guide, you’ll learn exactly how part geometry drives heat buildup, how to balance cure speed with thermal risk, and how to validate the ideal potting formulation for your specific application.
Let’s dive right in.
Quick Answer
A low exotherm epoxy potting compound is an encapsulation material formulated to control and reduce the internal heat generated during the chemical curing process. It is specifically engineered for deep-section potting, large-volume applications, and assemblies housing heat-sensitive electronic components.
- Controls Peak Temperatures: Moderates the internal exothermic reaction spike, safeguarding fragile semiconductors, sensors, and circuitry from thermal damage.
- Minimizes Shrinkage and Stress: Drastically lowers internal mechanical stress, preventing shrinkage voids, surface deformation, and micro-cracks.
- Enables Deep Single Pours: Allows large-mass and high-volume electronic encapsulation without the risk of thermal runaway.
What Buyers Need to Know First
Before sourcing a low exotherm epoxy potting compound, you need to look beyond basic technical data sheets. Standard lab ratings are often measured on thin, low-mass samples, which fail to reflect the real heat buildup inside deep enclosures.
When choosing an electronic encapsulation resin for large pours, keep these primary factors in mind:
- Total Mass and Depth: Chemical reactions accelerate with mass. A formula that stays cool in a 50-gram test can generate damaging peak temperatures in a 2-kilogram housing.
- Component Thermal Thresholds: Check the maximum temperature tolerances of your most delicate microchips, capacitors, and sensors before locking in a cure schedule.
- Cure Time Trade-Offs: A slow cure potting epoxy naturally releases heat at a controlled rate, reducing thermal shock at the expense of longer demolding times.
- Shrinkage and Stress: Excessive reaction heat increases shrinkage and residual stress, which can crack fragile solder joints or compromise moisture seals.
| Key Selection Factor | Critical Impact on Production |
|---|---|
| Pour Volume & Geometry | Drives the actual peak potting exotherm inside the casing. |
| Reaction Kinetics | Balances processing time against safe operating temperatures. |
| Substrate Adhesion | Ensures long-term protection without delamination caused by thermal stress. |
Getting the right deep potting epoxy system requires aligning material reactivity directly with your part dimensions and production cycle requirements.
Why Large Potting Volumes Generate Heat
When we formulate and pour an epoxy, the curing process relies on a natural exothermic chemical reaction. As polymer chains link together, they release heat. In standard assemblies with thin layers, this thermal energy escapes quickly into the surrounding air or enclosure walls.
In large volume potting, the dynamic changes completely:
- Internal Heat Trapping: Epoxy acts as a thermal insulator. In mass pours, heat generated at the center cannot escape easily, creating a hot core.
- Thermal Runaway: As the core temperature climbs, it accelerates the chemical reaction. This faster reaction produces even more heat, resulting in a sudden potting exotherm spike.
- Material Degradation: Uncontrolled internal heat can lead to shrinkage, internal stress cracking, air voids, and charring.
Controlling this thermal buildup is why selecting a dedicated low exotherm epoxy potting compound or a slow cure potting epoxy is critical for deep pours.
How Part Geometry Changes Exotherm
The physical shape of your housing directly dictates how effectively heat dissipates during the cure cycle. It comes down to the surface-area-to-volume ratio:
| Enclosure Profile | Heat Dissipation Rate | Exotherm Risk Level | Recommended Approach |
|---|---|---|---|
| Deep, narrow cavities | Low surface exposure; heat stays trapped | High | High-performance low heat potting epoxy |
| Wide, shallow trays | High surface area; rapid heat transfer | Moderate to Low | Standard or moderate-cure potting systems |
| Thick-walled plastic cases | Insulative; traps core heat inside | High | Custom filled or slow-reacting formulation |
| Metallic enclosures | Conductive; acts as an active heat sink | Low to Moderate | Balanced viscosity and cure profile |
For deep potting epoxy applications with tight, compact internal electronics, part geometry must be factored in early to ensure optimal electronic encapsulation resin performance without risking component burnout.
Component Temperature Risk
Excessive heat during cure poses a direct threat to sensitive electronics. When potting exotherm spikes uncontrollably, the internal core temperature can easily exceed the safe limits of delicate sub-assemblies.
Using a dedicated low exotherm epoxy potting compound protects against the most common thermal failure modes:
- Component degradation: Heat spikes can damage semiconductor junctions, warp plastic bobbins, or alter the values of sensitive passives.
- Solder joint reflow: High peak temperatures risk weakening or micro-fracturing internal solder connections.
- Internal stress and cracking: Rapid heat generation followed by uneven cooling creates severe shrinkage stress, leading to delamination and cracks in the cured matrix.
- Thermal sensor interference: Premature triggering or permanent drift of embedded thermal cutoffs and sensors during the cure cycle.
Selecting the right electronic encapsulation resin ensures consistent electronic component protection without subjecting the assembly to destructive cure temperatures.
Material and Cure-Speed Trade-Offs
Controlling peak temperatures almost always involves balancing reactivity against process time. Formulating for low heat generation directly influences cycle times, handling characteristics, and final mechanical properties.
| Parameter | Fast-Curing Systems | Low Exotherm Systems |
|---|---|---|
| Peak Exotherm | High (risks component damage) | Controlled / Low |
| Working Life / Pot Life | Short (minutes) | Extended (hours) |
| Cure Time | Rapid handling | Slow cure potting epoxy profile |
| Internal Shrinkage Stress | Significant | Minimal |
| Deep-Pour Capability | Limited to thin layers | Suitable for deep potting epoxy applications |
A slower reaction profile gives heat enough time to dissipate naturally, preventing localized hot spots in high-volume pours while keeping the structural integrity of the cured epoxy intact.
When Staged Potting Helps
When dealing with deep cross-sections or massive enclosures, even a low exotherm epoxy potting compound can reach elevated core temperatures if poured all at once. Staged potting—pouring material in successive layers—provides a controlled pathway to manage heat dissipation without sacrificing encapsulation integrity.
We recommend staged potting under the following conditions:
- Deep Potting Epoxy Requirements: Cavities exceeding 75–100 mm in depth where heat cannot escape through the housing walls quickly enough.
- High-Mass Assemblies: Pours requiring several liters of electronic encapsulation resin around sensitive active components.
- Interlayer Bonding Needs: Applying the second layer during the initial gel stage (the “tacky” phase) to ensure full chemical bonding without cold joints or seams.
- Minimizing Cure Shrinkage: Reducing mechanical stress on delicate solder joints and microelectronics by distributing volume contraction across multiple cure cycles.
| Potting Method | Peak Exotherm Control | Production Cycle Time | Best Suited For |
|---|---|---|---|
| Single-Stage Pour | Dependent strictly on resin chemistry | Fast (single gel & cure cycle) | Low-to-medium volumes (< 250 ml), shallow parts |
| Staged (Multi-Pour) | Maximum control (heat dissipates per layer) | Longer (multiple pour & set intervals) | Large volume potting, heavy assemblies, ultra-deep cavities |
How to Validate a Low-Exotherm Potting System
Validating a slow cure potting epoxy formulation requires real-world testing under actual production conditions. Bench-top data sheets only provide a baseline; the true thermal profile depends entirely on part mass, enclosure materials, and ambient conditions.
- Embed Core Thermocouples: Place temperature sensors at the geometric center of the casting mass and directly against the most heat-sensitive components to monitor real-time potting exotherm.
- Log the Thermal Curve: Record temperature spikes from initial mixing through gelation to identify peak exotherm values and verify they remain within safe component tolerances.
- Inspect for Internal Voids and Cracking: Cross-section the cured unit or use ultrasonic/X-ray inspection to check for shrinkage voids, air entrapment, or delamination.
- Verify Mechanical and Electrical Integrity: Run insulation resistance, dielectric strength, and thermal cycling tests to confirm complete cure and robust electronic component protection.
What Information Should You Send to RW ATELIER?
To help us recommend or develop the ideal low exotherm epoxy potting compound for your assembly, sharing your project parameters upfront speeds up validation and ensures reliable thermal management.
When you reach out to our team at RW ATELIER, providing the following technical details allows us to evaluate your exact potting exotherm and cure requirements:
- Potting Dimensions and Volume: Total pour mass, depth, and cavity geometry to evaluate peak exotherm risks during large volume potting.
- Housing and Substrate Materials: The composition of the enclosure (e.g., aluminum, plastic, FR4) to determine adhesion and heat dissipation pathways.
- Component Temperature Limits: The maximum peak temperature threshold that your most sensitive electronics can tolerate during cure.
- Operating Environment: Long-term service temperatures, thermal shock exposure, humidity, and chemical resistance requirements for the electronic encapsulation resin.
- Process & Dispensing Setup: Your target gel time, demold window, mixing method (manual batching or meter-mix dispensing), and whether you require a custom epoxy formulation.
| Key Project Detail | Why We Need It |
|---|---|
| Pour Depth & Mass | Calculates thermal mass and prevents runaway heat buildup. |
| Component Thresholds | Sets the hard ceiling for allowable peak exothermic reaction. |
| Production Cycle Targets | Balances slow cure potting epoxy chemistry with your throughput needs. |
| Environmental Demands | Ensures finished dielectric strength, adhesion, and physical durability. |
How Can RW ATELIER Support This Project?
As a specialized manufacturer, we work directly with engineering and production teams worldwide to supply dependable resin systems tailored to demanding assembly requirements. When standard materials generate too much heat or fail under thermal stress, we step in with direct manufacturing capabilities and dedicated technical support.
End-to-End Support Capabilities
- Custom formulation services: We tailor reactivity, cure profiles, and viscosity to match specific depth, volume, and cycle-time constraints.
- Factory-direct supply: As an OEM and bulk supplier, we deliver consistent material quality straight from our production lines to your facility.
- Application matching: We align the right resin chemistry with your assembly geometry, protecting sensitive internal components from heat spikes and curing stress.
- Scalable production batches: From early pilot testing quantities to full-scale commercial manufacturing, our capacity scales with your output needs.
Our direct-from-factory structure ensures you get precise material performance, stable batch-to-batch consistency, and dependable delivery for all industrial-scale assembly projects.
